


Validation & Compliance
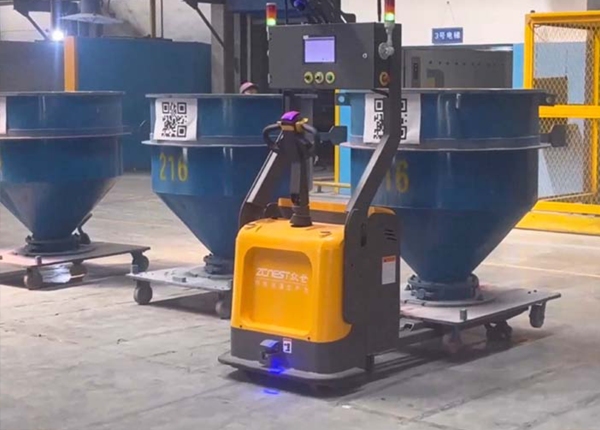
Pharmaceutical warehouses must maintain absolute control over inventory. In these highly regulated environments, ZCNEST AMR forklifts automate pallet transport while ensuring 100% data integrity for 2026 standards.
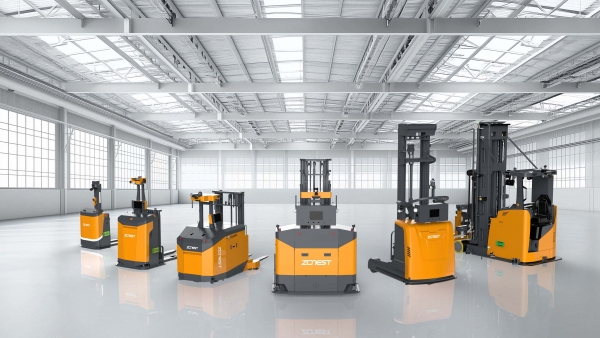
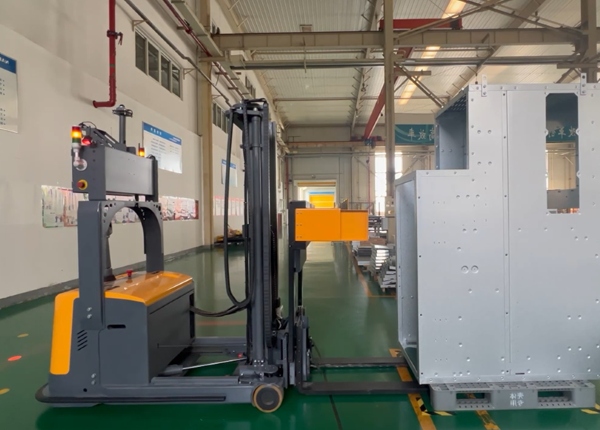
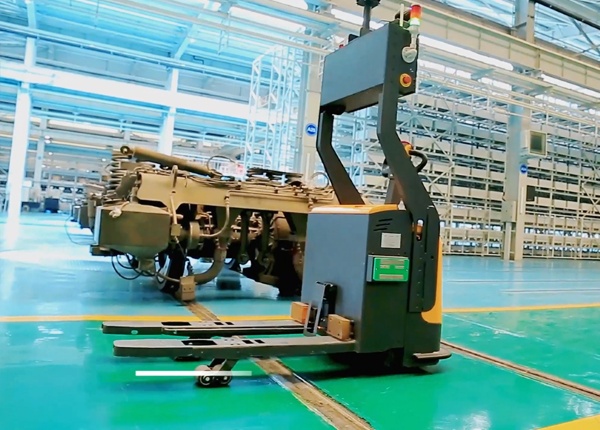
Autonomous forklifts operate according to validated programmed routes and handling protocols. This mechanical consistency helps ZCNEST users maintain rigorous material handling standards, essential for sensitive medical supplies.
Because ZCNEST robotic forklifts integrate directly with warehouse management systems, every single pallet movement is recorded digitally. This creates an unshakeable audit trail, improving end-to-end visibility throughout the global pharmaceutical supply chain.
Automation eliminates the inherent risks of human handling errors. For life-science companies, this reliability is not just an efficiency gain—it is a critical requirement to maintain compliance with strict industry regulations and safeguard product integrity.












 Chinese
 English





